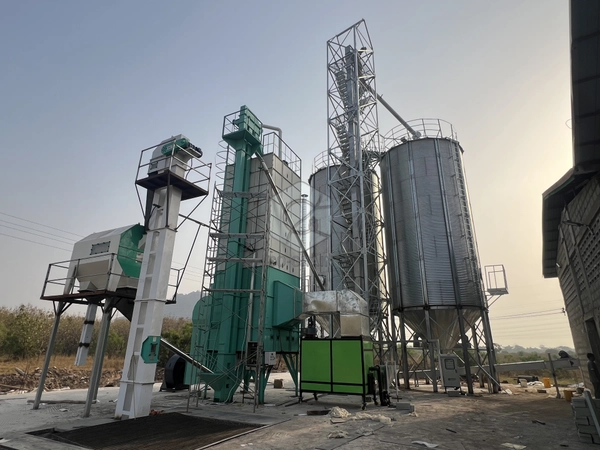
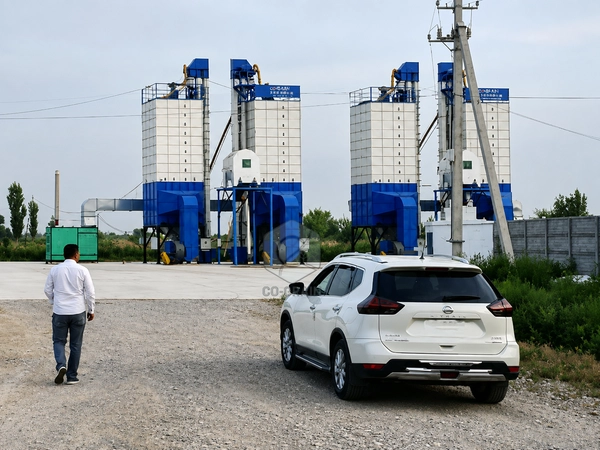
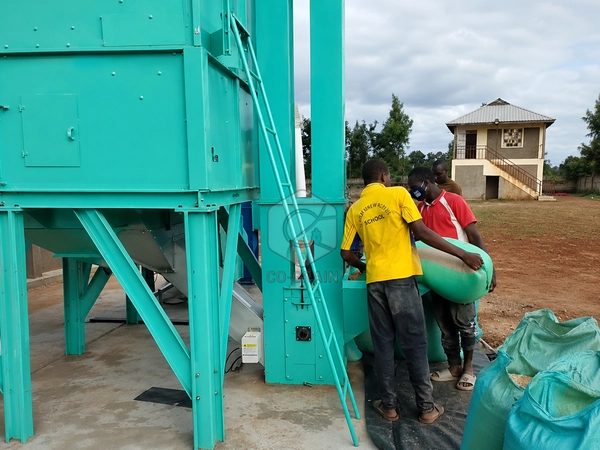
The right grain conveyor depends on more than capacity. A commercial grain plant may use different equipment for vertical lifting, horizontal transfer, silo filling, dryer feeding and short-distance discharge. The best choice matches the route, grain characteristics and complete plant layout.
Quick Conveyor Selection
Why Conveyor Selection Matters
Conveying equipment connects every major section of a grain plant. A typical route may be:
If the equipment is selected without considering the complete process, the plant may suffer capacity bottlenecks, grain damage, blockage, excessive dust, unstable dryer feeding, poor silo filling, high maintenance and unnecessary energy use.
Define the Conveyor Duty First
Before choosing a model, identify what the conveyor must do:
- Lift grain vertically through a major elevation difference
- Move grain horizontally over a short or long distance
- Feed a dryer or another machine at a controlled rate
- Fill several silos or collect grain from multiple silos
- Handle wet paddy, fragile seed or other sensitive materials
- Operate in a dusty, outdoor or weather-sensitive environment
Equipment by Application
Bucket Elevator
Evaluate it first when grain needs major vertical lifting with a compact footprint.
- Receiving pit to cleaner
- Wet buffer to dryer
- Dryer discharge to silo top
- Silo discharge to processing
Drag Chain Conveyor
A practical option for enclosed horizontal conveying and routes with multiple inlets or outlets.
- Silo-top filling
- Silo-bottom collection
- Dryer-to-elevator transfer
- Compact grain plant layouts
Belt Conveyor
Often preferred for medium-to-long horizontal transfer and relatively gentle handling of paddy or seed.
- Grain yard transfer
- Dryer-to-storage transfer
- Truck loading
- Long silo-area routes
Enclosed Belt Conveyor
Combines belt conveying with added protection for outdoor routes, galleries and weather-sensitive installations.
- Rain protection
- Dust containment
- Cleaner plant environment
Air Cushion Belt Conveyor
Designed for selected long-distance or high-capacity routes where a supported belt can reduce rolling resistance.
- Long silo galleries
- Large grain storage projects
- Grain terminals
Screw Conveyor
Useful for short-distance transfer, hopper discharge, bin feeding and compact equipment connections.
- Controlled machine feeding
- Short silo-bottom discharge
- Compact process layouts
Inclined Chain Conveyor
Can combine horizontal conveying and moderate elevation change where a separate elevator would use too much space.
- Receiving pit to elevated equipment
- Dryer feeding
- Compact enclosed routes
Quick Comparison
| Application | Equipment to evaluate | Main reason |
|---|---|---|
| Major vertical lift | Bucket Elevator | High lift with a compact footprint |
| Enclosed horizontal transfer | Drag Chain Conveyor | Multiple inlets, outlets and silo routes |
| Long gentle transfer | Belt Conveyor | Continuous flow with reduced impact |
| Protected outdoor route | Enclosed Belt Conveyor | Rain and dust protection |
| Long high-capacity gallery | Air Cushion Belt Conveyor | Selected long-distance projects |
| Short compact feeding | Screw Conveyor | Simple hopper or bin connection |
| Horizontal plus incline | Inclined Chain Conveyor | Combined transfer and elevation change |
Selection Factors
Typical Project Arrangements
Bucket Elevator → Drag Chain Conveyor → Silo 1 / Silo 2 / Silo 3 / Silo 4
Multiple discharge points and an enclosed silo-top route make this arrangement practical.
Grain Dryer → Bucket Elevator → Long Belt Conveyor → Silo Storage
For very long or high-capacity routes, an Air Cushion Belt Conveyor may also be evaluated.
Silo Outlet → Screw Conveyor → Bucket Elevator / Processing
A short and compact route can make a Screw Conveyor a suitable choice.
Silo 1 / Silo 2 / Silo 3 / Silo 4 → Drag Chain Conveyor → Bucket Elevator
The multiple-inlet requirement favors an enclosed Drag Chain Conveyor.
Receiving → Bucket Elevator → Cleaner → Belt Conveyor → Buffer / Dryer
Dryer → Belt Conveyor → Paddy Storage
A Simple Decision Path
Bucket Elevator
Screw Conveyor
Drag Chain
Belt Conveyor
Air Cushion Belt
Inclined Chain
Common Selection Mistakes
- Using one conveyor type for every route
- Selecting only by T/H without checking distance and layout
- Ignoring moisture, grain damage and transfer impact
- Using a Screw Conveyor for a very long route
- Ignoring multiple silo inlets and outlets
- Leaving no access for inspection and maintenance
- Designing the conveyors only after the plant layout is finalized
Frequently Asked Questions
Which conveyor is best for grain?
There is no single best type. Bucket Elevators suit vertical lifting, Drag Chain Conveyors suit enclosed horizontal transfer, Belt Conveyors suit longer gentle routes, and Screw Conveyors suit short feeding duties.
What is the best conveyor for paddy?
Belt Conveyors are often worth evaluating for relatively gentle long-distance paddy handling. Bucket Elevators and Drag Chain Conveyors can still be used where the route requires them.
What conveyor should I use for grain silos?
A typical system uses Bucket Elevators for vertical lifting and Drag Chain, Belt or Air Cushion Belt Conveyors for silo-top distribution.
What conveyor should I use under silos?
Drag Chain Conveyors are commonly suitable for collecting from multiple silos. Screw Conveyors can be useful for selected short-distance discharge duties.
Does conveyor speed affect grain damage?
Yes. Excessive speed and poor transfer design can increase impact and breakage, especially for paddy and seed.
Do enclosed conveyors eliminate dust?
No. They reduce exposure, but loading and discharge points may still require aspiration and dust collection.
Key Takeaway
Choose the conveyor according to the duty, route and material, rather than using one machine everywhere. The most reliable grain plants combine Bucket Elevators, Drag Chain Conveyors, Belt Conveyors, Air Cushion Belt Conveyors, Screw Conveyors and Inclined Chain Conveyors where each one fits best.
Co-Grain evaluates capacity, distance, elevation, grain quality, dust control, energy use, maintenance and the complete plant layout to develop a practical grain conveying solution.
Discuss Your Project
Need a Complete Grain Drying & Storage Solution?
Co-Grain provides turnkey grain drying plants, grain storage silos, cleaning, conveying, and automation systems for modern grain handling facilities. Our equipment includes batch and continuous grain dryers, paddy dryers, grain cleaners, bucket elevators, chain conveyors, and belt conveyors.
From engineering design and equipment manufacturing to installation and commissioning, we deliver reliable, customized solutions for paddy rice, maize, wheat, barley, sorghum, and other grains.
Talk to Co-Grain
Planning a new project or upgrading an existing facility? Contact us for a customized solution and free quotation.
Henan Co-Grain Machinery Engineering Co., Ltd.
Email: info@ricemillplants.com
WhatsApp: 0086 18339828199