Discover how grain bucket elevators work, including their working principles, main components, conveying capacity, and applications in modern grain handling systems. Learn how bucket elevators efficiently transport paddy rice, corn, wheat, barley, soybeans, and other bulk grains vertically in grain drying plants, storage silos, rice mills, and grain processing facilities. Explore essential selection factors such as elevator capacity, lifting height, bucket design, belt or chain type, motor power, and grain characteristics, and understand how bucket elevators integrate with grain receiving, cleaning, drying, conveying, and silo storage systems to improve material handling efficiency, reduce grain damage, and ensure reliable continuous operation.
A grain bucket elevator is a vertical conveying machine used to lift paddy, corn, wheat and other bulk grains between receiving, cleaning, drying, storage and processing equipment. Its enclosed casing and continuous buckets provide a compact route when a plant needs to overcome a large elevation difference.
What Is a Grain Bucket Elevator?
A grain bucket elevator uses a continuous belt or chain fitted with buckets inside an enclosed casing. Grain enters the boot, is collected by the moving buckets, lifted vertically and discharged at the head into a downstream chute or conveyor.
Bucket elevators are common in commercial grain plants because cleaners, dryers, silos and milling machines are often installed at different elevations. The elevator solves the vertical part of the route within a relatively small footprint.
How Does a Bucket Elevator Work?
A motor and drive unit circulate the belt or chain around the boot and head. The buckets fill at the lower inlet, carry grain upward and discharge it as they pass around the head pulley or sprocket.
The cycle repeats continuously. Elevator capacity must be coordinated with the upstream conveyor and the downstream cleaner, dryer, silo conveyor or processing line.
Main Components
Boot section and inlet
The lower section receives grain and contains the bottom pulley or sprocket, tensioning arrangement, inspection access and cleanout points.
Buckets
Bucket size, shape, spacing and material affect capacity, filling behavior and grain handling quality.
Belt or chain
The continuous traction element carries the buckets. Selection depends on capacity, height, grain, speed and duty.
Elevator casing
Vertical casing sections enclose the buckets, contain dust, protect moving parts and provide support for access and monitoring components.
Head section
The head contains the drive pulley or sprocket, bearings, discharge section and inspection access.
Drive and tensioning
Motor, gearbox, coupling, backstop and tensioning keep the belt or chain moving steadily under load.
Why Use a Bucket Elevator?
The main reason is vertical lift. A horizontal conveyor can move grain across distance, but a long inclined route would require much more floor space to reach a silo roof or elevated machine.
| Item | Bucket elevator | Belt conveyor |
|---|---|---|
| Main direction | Vertical | Horizontal or inclined |
| Typical footprint | Compact | Longer route |
| Carrying method | Buckets on belt or chain | Continuous belt |
| Typical duty | Ground level to silo roof | Long horizontal transfer |
| Common combination | Elevator + top conveyor | Conveyor + elevator |
Bucket elevators and belt conveyors perform different duties and are normally combined rather than treated as competing machines.
Applications in Grain Plants
Receiving and pre-cleaning
Truck → receiving pit → drag chain or belt conveyor → bucket elevator → rotary, vibrating or drum cleaner.
Grain dryer feeding
Wet-grain buffer → controlled conveyor → bucket elevator → grain dryer inlet.
Dryer discharge and silo filling
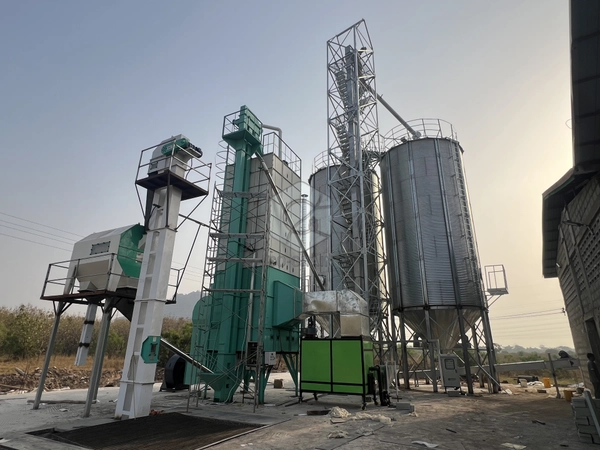
Grain dryer → horizontal conveyor → bucket elevator → silo-top chain or belt conveyor → multiple silos.
Silo discharge and processing
Silo outlet → bottom drag chain, screw or belt conveyor → bucket elevator → rice mill, flour mill, feed mill or truck loading.
Inside a rice mill, elevators can connect the paddy cleaner, destoner, husker, paddy separator, whitener, polisher, grader and packaging sections.
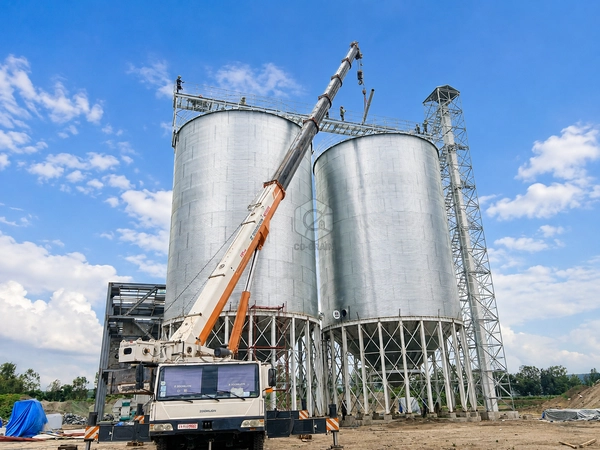
Bucket Elevator for Silo Filling
A common multi-silo arrangement is:
The elevator provides the vertical lift; the top conveyor, gates and distributors provide horizontal distribution. One elevator can serve several silos when capacity, discharge points, level sensors, supports and automation logic are confirmed.
The elevator itself does not choose the destination. Route-control equipment above the silos performs that function.
How to Choose Bucket Elevator Capacity
Capacity is normally specified in tons per hour, but T/H alone is not enough. Confirm the complete operating basis:
- Grain type, bulk density and moisture
- Required T/H and peak receiving rate
- Vertical lift and discharge elevation
- Bucket size, spacing and belt or chain speed
- Inlet and discharge conditions
- Upstream and downstream equipment capacity
- Indoor or outdoor installation and operating hours
For example, a receiving system may need to handle 40 T/H at harvest peaks while the dryer operates at 10 T/H. A wet-grain buffer can separate these two operating conditions, but the receiving elevator must still be selected for its own required flow.
Grain Quality, Inlet and Discharge Design
Paddy, seed and other damage-sensitive grains require attention to bucket speed, bucket shape, inlet loading, transfer chute, drop height and discharge geometry.
- Controlled feeding into the boot
- Even bucket filling
- Reduced rebound and impact at the head
- Sealed chutes and suitable aspiration points
- Cleanout access for wet grain and impurities
Higher speed may increase capacity, but it can also affect grain impact, belt load, power and wear. The correct speed should follow the selected elevator design rather than being chosen from motor power alone.
Safety Monitoring and Maintenance
A commercial grain elevator may use speed-loss monitoring, belt misalignment sensors, bearing temperature monitoring, motor overload protection, boot blockage detection, emergency stops and access-door safety provisions. These signals can be integrated into the plant PLC.
Routine inspection points
- Buckets, fasteners and belt or chain
- Head and boot pulleys or sprockets
- Bearings, drive and tensioning system
- Casing, inspection doors and chutes
- Speed, alignment and temperature sensors
Start-up normally begins with downstream equipment, followed by the elevator and then the grain feed. Shutdown normally stops grain feeding first and allows the route to clear according to the approved control sequence.
Frequently Asked Questions
What grains can a bucket elevator handle?
Depending on its design, it can handle paddy, corn, wheat, barley, sorghum and other confirmed bulk grains.
Can a bucket elevator fill a grain silo?
Yes. It lifts grain to the silo roof, where a top conveyor distributes it to one or more silos.
Can a bucket elevator feed a grain dryer?
Yes. It can lift wet grain from a buffer silo or conveyor to the dryer inlet when its capacity and inlet arrangement match the dryer.
Is a bucket elevator better than a belt conveyor?
They perform different duties. Bucket elevators are mainly for vertical lifting; belt conveyors are mainly for horizontal or inclined transfer.
What safety sensors can be used?
Depending on the project, speed, misalignment, bearing temperature, blockage and motor-overload monitoring may be included.
Key Takeaway
A bucket elevator is one of the core machines connecting grain receiving, cleaning, drying, storage and processing. Co-Grain selects it according to grain type, capacity, moisture, lift height, upstream conveyor, downstream conveyor, silo layout, maintenance access, monitoring and automation requirements.
Discuss Your Project
Need a Complete Grain Drying & Storage Solution?
Co-Grain provides turnkey grain drying plants, grain storage silos, cleaning, conveying, and automation systems for modern grain handling facilities. Our equipment includes batch and continuous grain dryers, paddy dryers, grain cleaners, bucket elevators, chain conveyors, and belt conveyors.
From engineering design and equipment manufacturing to installation and commissioning, we deliver reliable, customized solutions for paddy rice, maize, wheat, barley, sorghum, and other grains.
Talk to Co-Grain
Planning a new project or upgrading an existing facility? Contact us for a customized solution and free quotation.
Henan Co-Grain Machinery Engineering Co., Ltd.
Email: info@ricemillplants.com
WhatsApp: 0086 18339828199
Discuss Your Project
Need a Complete Grain Drying & Storage Solution?
Co-Grain provides turnkey grain drying plants, grain storage silos, cleaning, conveying, and automation systems for modern grain handling facilities. Our equipment includes batch and continuous grain dryers, paddy dryers, grain cleaners, bucket elevators, chain conveyors, and belt conveyors.
From engineering design and equipment manufacturing to installation and commissioning, we deliver reliable, customized solutions for paddy rice, maize, wheat, barley, sorghum, and other grains.
Talk to Co-Grain
Planning a new project or upgrading an existing facility? Contact us for a customized solution and free quotation.
Henan Co-Grain Machinery Engineering Co., Ltd.
Email: info@ricemillplants.com
WhatsApp: 0086 18339828199